

SeamData
Description
Section titled “Description”Defines the start and end phase data of a welding seam. Allows detailed specification of timing and arc conditions across three phases: Ignition, Heat, and End. Typically, the same values are maintained for an entire seam or across multiple seams.
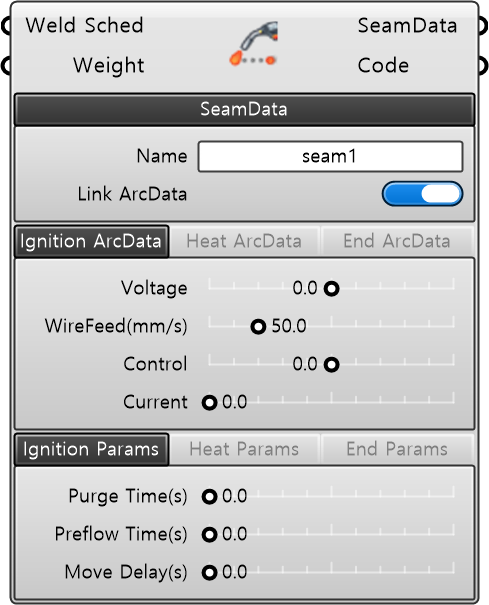
| Name | Type | Description |
|---|---|---|
| Weld Sched | Weld Sched | The welding program number (schedule) and welding mode to be utilized. |
| Weight | Number | Weight factor applied to wirefeed1. |
Required Parameter
Section titled “Required Parameter”| Name | Type | Description |
|---|---|---|
| Name | String | Variable name. |
| Link ArcData | Boolean | Links ArcData values across all sequences (Ignition, Heat, End). TRUE: Adjusting parameters in one phase automatically syncs the others. FALSE: Allows independent tracking for each phase (Default). |
| Name | Type | Description |
|---|---|---|
| Voltage | Number | Welding voltage (ABB convention). For Fronius TPS/TPS-i: Adjusts the arc length. |
| Wirefeed(m/min) | Number | Wire feed speed (m/min). Common to both ABB and Fronius systems. |
| Control | Number | Control parameter (ABB convention). For Fronius TPS/TPS-i: Adjusts dynamic characteristics. |
| Current | Number | Welding current (ABB convention). Not utilized in Fronius TPS/TPS-i setups. |
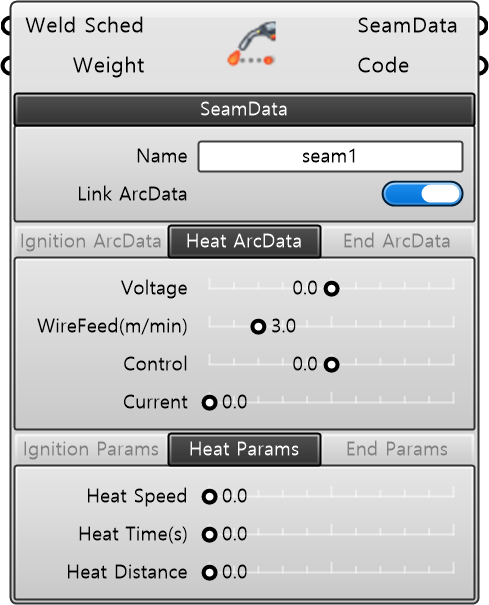
| Name | Type | Description |
|---|---|---|
| Voltage | Number | Welding voltage (ABB convention). For Fronius TPS/TPS-i: Adjusts the arc length. |
| Wirefeed(m/min) | Number | Wire feed speed (m/min). Common to both ABB and Fronius systems. |
| Control | Number | Control parameter (ABB convention). For Fronius TPS/TPS-i: Adjusts dynamic characteristics. |
| Current | Number | Welding current (ABB convention). Not utilized in Fronius TPS/TPS-i setups. |
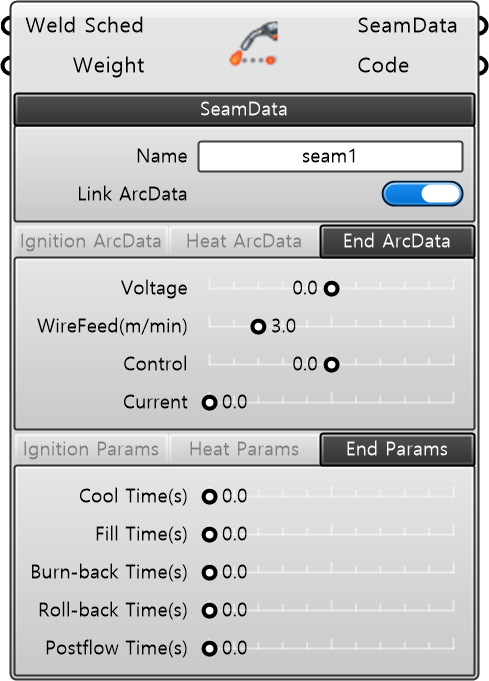
| Name | Type | Description |
|---|---|---|
| Purge Time | Number | Gas pre-purge duration (s) required to fill the gas line and weld torch. If travel time to the start position is shorter than the purge time, the robot dwells at the start position until the timer expires. |
| Purgeflow Time | Number | Shielding gas pre-flow duration (s) over the weldment. The robot remains stationary at the ignition location during this window before the arc is initiated. |
| Move Delay | Number | Dwell time delay (s) from the point of arc stabilization at ignition until the primary heating phase begins. |
| Name | Type | Description |
|---|---|---|
| Heat Speed | Number | Travel speed maintained during the initial heating sequence at the start of welding. |
| Heat Time | Number | Duration (s) for the initial heating sequence. Active only when Heat Distance or Heat Speed is set to 0. |
| Heat Distance | Number | Linear distance over which the specified heating configuration is applied at the beginning of the weld segment. |
| Name | Type | Description |
|---|---|---|
| Crater Time | Number | Duration (s) allocated for crater filling during the termination phase of the weld. |
| Burnback Time | Number | Additional arc burn time (s) sustained after wire feed termination to prevent the electrode wire from sticking in the solidification matrix of the weld pool. |
| Postflow Time | Number | Gas post-flow duration (s) supplied after arc termination to protect the cooling crater weldment from atmospheric oxidation. |
Output
Section titled “Output”| Name | Type | Description |
|---|---|---|
| SeamData | SeamData | Outputs the configured ABB SeamData configuration stream. |
| Code | String | Outputs the compiled RAPID instruction code. |